A stainless fastener that turns freely for four threads and then seizes solid has not necessarily met a bad part. Galling is a property of the joint — the mating materials, the thread geometry, the surface condition, the manufacturing variation, the lubrication or coating, and the way the joint was assembled. One anti-galling note on a drawing rarely changes any of them.
One consequence is worth stating up front: lubrication changes the torque–tension relationship. It cannot be added while assuming an existing dry torque specification still holds.
What Stainless Steel Thread Galling Actually Is
Galling is severe adhesive wear. As loaded thread flanks slide during tightening or removal, microscopic contact points deform, adhere, and transfer material between the mating surfaces. Friction rises, surface damage accelerates, and the joint can seize before it reaches its intended position or preload. “Cold welding” is the common shorthand, though a galling event is not necessarily a complete metallurgical weld across the interface.
The warning signs — rough or jerky rotation, a sudden rise in installation torque, torn thread surfaces, visible transferred metal, seizure during tightening, damage during disassembly — are all suggestive and none is conclusive. Dimensional error, contamination, damaged lead threads, misalignment, or simply the wrong mating part produce similar symptoms.
Why Austenitic Stainless Threads Are Susceptible
Common austenitic grades such as 304 and 316 combine high ductility with a tendency toward adhesive material transfer under unfavorable sliding contact. Local contact pressure deforms thread asperities, and continued sliding disrupts the surface film. Adhesion, material transfer, plastic deformation, and the work hardening that follows then accelerate the damage. Similar mating materials in similar surface conditions make the cycle worse.
The molybdenum addition in 316 improves resistance to localized corrosion, particularly pitting and crevice corrosion in chloride-containing environments. It does not make 316 more resistant to galling than 304. Corrosion resistance and galling resistance are separate selection criteria — see our stainless steel page for grade selection on the corrosion side.
Diagnose the Failure Before Changing the Part
| Observed condition | Likely mechanism | Common contributors | What to verify |
|---|---|---|---|
| Rapid friction increase, torn surfaces, transferred metal, seizure | Adhesive galling | Similar material and surface conditions, insufficient hardness differential, high contact pressure, inadequate lubrication, rapid engagement | Material condition, surface damage, lubricant state, assembly record |
| Thread will not start correctly or enters at an angle | Cross-threading | Misalignment, damaged lead, poor access, incorrect mating part | Axis alignment, lead threads, size and pitch |
| Thread crests or flanks shear away | Stripping | Insufficient shear area, weak material, inadequate engagement, overload | Engagement, material strength, thread geometry, applied load |
| Damage after repeated small-amplitude motion | Fretting wear | Joint movement, insufficient clamp load, vibration at the interface | Joint stiffness, preload retention, movement pattern |
| Pits, rust staining, deposits, or attack in shielded areas | Corrosion | Chlorides, trapped moisture, galvanic coupling, contamination | Environment, drainage, grade, cleaning, mating materials |
| Tight or erratic rotation without adhesive transfer | Debris binding or dimensional error | Chips, burrs, coating buildup, poor concentricity, tool wear | Cleanliness, thread inspection, coating allowance, mating dimensions |
Visual inspection is where the investigation starts, not where it finishes. A seized assembly often involves more than one mechanism — contamination can initiate binding before adhesive damage develops.
Material Pairing and Hardness Strategy
Identical or similarly conditioned austenitic stainless surfaces are vulnerable when load and sliding conditions favor adhesion. The options are a greater hardness differential, a different stainless family, a compatible non-stainless mating material, a surface treatment, or a threaded insert — each of which still has to meet the joint’s strength, corrosion, temperature, and cleanliness requirements.
“Always use dissimilar metals” is not a safe design rule. A material change can introduce galvanic corrosion, incompatible thermal expansion, reduced thread strength, metallic contamination, or poor behavior at service temperature. Review the mating assembly, not one component in isolation.
A well-chosen insert gives a replaceable wear interface where a stainless component will be opened repeatedly. It also consumes wall thickness and brings installation, retention, corrosion, and inspection requirements with it. Vacuum and cleanroom applications restrict insert style, locking features, lubricants, and trapped volumes further.
Design Threads for Manufacturing and Assembly
Specify the governing thread system clearly. Unified inch threads are commonly defined under ASME B1.1; metric threads may follow ASME B1.13M or the applicable ISO metric thread standards. Do not mix ASME and ISO tolerance designations without confirming dimensional and inspection compatibility. The drawing should identify nominal size, pitch, tolerance class, usable thread depth, and inspection requirements. There is no universal “anti-galling” thread class — the right fit depends on the governing standard, thread size, finish, load, and service conditions.
Details worth settling before release:
- Provide an entry chamfer that supports alignment without removing necessary thread engagement.
- Protect lead threads from burrs and handling damage.
- Provide adequate thread runout or tool-relief space where the geometry permits.
- Separate drill depth, full-thread depth, and usable engagement in blind holes.
- Provide chip clearance in blind holes, and define how machining fluid and cleaning residues will be removed.
- Check concentricity and alignment between mating components.
- Account for coating buildup or electropolishing material removal when defining pre-process dimensions and final thread fit.
Longer engagement does not increase joint strength indefinitely. Once another feature governs load capacity, extra thread length only adds machining time and assembly exposure.
CNC Machining and Finishing Considerations
Tapped, thread-milled, and single-point-machined threads can all be appropriate in custom stainless parts. Tapping is efficient, with tool wear, chip control, synchronization, and blind-hole depth to watch. Where the geometry gives enough tool access, thread milling reduces chip packing and allows controlled size adjustment.
Tool condition drives flank form, pitch diameter, burr formation, and consistency. Plan inspection around the specified thread standard and the functional requirement rather than around what is convenient to gauge.
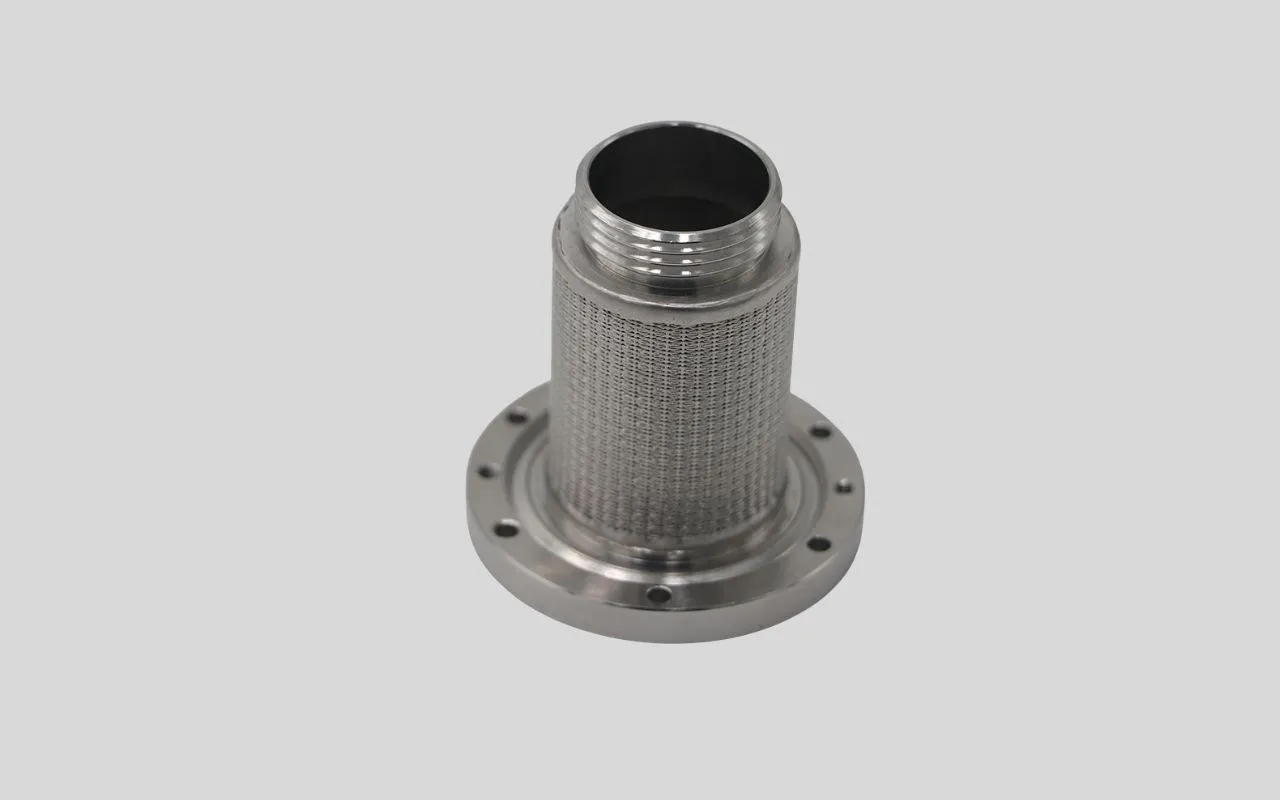
Deburr without rolling material into the thread, keep lead threads clean, and control carbon-steel contamination during machining and handling. Rolled external threads offer favorable surface and mechanical characteristics on some fasteners, but rolling is not a universal option for custom CNC geometry and does not apply to internal threads.
Lubrication Changes Both Galling Risk and Preload
A compatible lubricant or anti-seize reduces friction and interrupts adhesive contact. It also changes how much clamp load a given torque produces, which is why dry and lubricated torque specifications are not interchangeable. If preload matters, define the lubrication condition and validate the tightening method with the actual thread, finish, mating materials, and lubricant. Applying anti-seize to an unchanged dry torque value is a preload error waiting to happen.
Conventional compounds are prohibited outright in oxygen service, vacuum systems, semiconductor and cleanroom equipment, food-contact systems, medical devices, and other contamination-sensitive applications. Approval may depend on outgassing, extractables, chemical compatibility, particles, temperature, cleaning, and the customer’s approved-material list. Labels such as “food grade” or “vacuum compatible” do not establish suitability for a specific application.
Coatings, Inserts, Passivation, and Electropolishing
These treatments solve different problems, and they are not substitutes for one another:
- Dry-film or anti-friction coatings reduce friction without a wet assembly lubricant. Verify thickness, internal-thread uniformity, wear life, temperature capability, cleanliness, and final fit.
- Diffusion or low-temperature hardening treatments improve surface hardness and adhesive-wear behavior, and can alter corrosion resistance, dimensions, or material properties.
- Selected metallic coatings change the mating interface, and with it fit, galvanic compatibility, temperature performance, and contamination control.
- Chemical passivation removes free iron and other exogenous contamination and supports the corrosion performance of a properly selected grade. ASTM A967/A967M covers passivation treatments and verification; it is not a galling-prevention procedure.
- Electropolishing improves cleanliness, cleanability, and corrosion behavior in suitable applications. Because it removes material, pre-process allowance and final thread inspection have to be defined. It does not guarantee galling-free assembly.
Assembly Practices That Reduce Risk
- Confirm the mating parts have the correct thread form, size, pitch, and material condition.
- Clean and inspect both threads before assembly; do not force damaged or contaminated parts together.
- Align the axes and start the thread by hand where access and safety permit.
- Use a controlled tightening speed, and avoid high-speed impact engagement on a joint that has not been validated for it.
- Apply only the approved lubricant or coating condition, consistently and in the specified location.
- Use calibrated tooling when torque or preload is controlled.
- Stop when resistance becomes abnormal. Driving a binding joint turns a recoverable alignment or debris problem into permanent thread damage.
- For joints opened repeatedly, define inspection or replacement criteria for the wear interface.
Corrosion Around Stainless Steel Threaded Joints
A joint can resist galling and still corrode, or resist corrosion and still gall. Shielded threads retain chlorides, cleaning residues, deposits, and moisture, creating crevice conditions; blind holes with poor drainage are especially hard to rinse and dry. Dissimilar mating materials that reduce adhesive interaction may create a galvanic couple in an electrolyte.
Corrosion control may need a grade suited to the chemical and temperature environment, drainage or cleaning access, contamination control, galvanic review, and a specified cleaning and passivation process. Passivation cannot compensate for an unsuitable alloy in a severe chloride environment.
Where a threaded component carries sustained tensile stress in a chloride-containing environment, the material, stress state, temperature, concentration, and exposure condition may also warrant a stress-corrosion-cracking assessment. Chloride exposure alone does not establish that cracking will occur.
Engineering Decisions by Service Condition
| Situation | Primary concern | Options to evaluate | Engineering caution |
|---|---|---|---|
| One-time controlled assembly | Reaching intended preload without seizure | Verified fit, clean threads, compatible lubricant, controlled installation | Qualify the production assembly condition and method |
| Frequent disassembly | Accumulated surface damage | Insert, replaceable mating part, coating, maintenance lubrication | Define inspection and replacement criteria |
| Dry assembly required | Adhesive contact without wet lubricant | Material or hardness differential, dry-film treatment, revised fit | Validate friction, wear life, cleanliness, and preload method |
| Vacuum or cleanroom service | Outgassing and particles | Approved dry treatment, compatible insert, controlled cleaning | Check approved-material list, trapped volumes, post-process cleanliness |
| Chloride exposure | Pitting and crevice corrosion | Suitable stainless grade, drainage, cleaning access, compatible pairing | Galling-resistant material choices may not meet the corrosion need |
| High-temperature service | Lubricant breakdown and property changes | Temperature-rated pairing, coating, or lubricant | Check oxidation, thermal expansion, preload relaxation, process limits |
| Thin-wall CNC component | Parent-thread strength and insert space | Optimized engagement, local boss, suitable insert | Check wall thickness, breakout risk, distortion, installation load |
What to Include in the Drawing or RFQ
“Stainless steel thread” is not enough for a reliable manufacturing and assembly review. Provide:
- stainless steel grade, material condition, and mating-part material;
- thread standard, nominal size, pitch, tolerance class or fit requirement;
- thread depth, usable engagement, entry, and runout requirements;
- expected assembly and disassembly cycles;
- target preload or controlled-torque requirement;
- dry, lubricated, or coated assembly condition;
- approved and prohibited lubricants or process materials;
- coating, hardening, passivation, electropolishing, or masking requirements;
- required dimensions and inspection condition before and after coating, hardening, or electropolishing;
- corrosion environment and service-temperature range;
- vacuum, cleanroom, oxygen, food, medical, or contamination restrictions;
- cleaning requirements, insert specifications, inspection criteria, and any material certificates, certificates of conformance, or inspection reports the purchase order requires;
- prototype, batch, and annual quantities.
What to include in a CNC machining drawing and RFQ covers the rest of the submission package.
Treat the Joint as the Design, Not the Thread
The thread is one element of a system that also includes the mating part, the surface condition, the lubricant, and the person or machine doing the tightening. Galling problems that survive a change of thread class usually survive it because the change addressed the only part of that system that was already fine.
Frequently Asked Questions
Does 316 stainless steel gall less than 304?
Not necessarily. The molybdenum in 316 improves resistance to pitting and crevice corrosion in many chloride environments, but galling depends on the complete sliding interface. Select the grade for the corrosion environment, then evaluate material condition, pairing, thread fit, lubrication, and assembly separately for galling risk.
Does passivation prevent stainless steel thread galling?
No. Chemical passivation removes free iron and other exogenous contamination and supports corrosion performance. It does not create a low-friction or wear-resistant thread interface. Galling control may require changes to material pairing, thread fit, surface treatment, lubrication, or assembly.
Can dimensional inspection predict galling?
No. Thread gauging verifies only what the selected method covers. A GO/NO-GO functional gauge does not independently confirm every thread element, and pitch-diameter measurement alone does not verify lead, flank form, alignment, or surface condition. Inspection is necessary, but galling depends on the complete joint and the assembly process.
References
- Nickel Institute — Review of Wear and Galling Characteristics of Stainless Steel
- Nickel Institute — Stainless Steel Fasteners: A Systematic Approach to Their Selection
- ASME B1.1-2024, Unified Inch Screw Threads
- ASME B1.13M-2005 (S2025), Metric Screw Threads: M Profile
- ISO 965-1:2026, ISO General Purpose Metric Screw Threads — Tolerances — Part 1
- ASTM A967/A967M-25, Chemical Passivation Treatments for Stainless Steel Parts
- ASTM B912-26, Passivation of Stainless Steels Using Electropolishing